Cutting affects leather consumption, edge quality and fit with the buckle. For a belt programme, the useful comparison is the cost and output of acceptable parts from the actual material mix. A machine’s advertised positioning accuracy or a single fast cutting cycle cannot establish that result.
A hydraulic clicker press cuts with a shaped die. A CNC digital cutter follows a programmed path with suitable tooling, which can include a knife. Both can serve leather goods production. The belt production workflow also includes preparation, finishing and assembly, which should be considered when comparing throughput.
This guide examines mechanics, nesting, dimensions, tooling and order volume. It uses equipment-manufacturer information to explain the available approaches, without assigning universal prices, scrap rates or performance guarantees to an entire class of machines.
Was sind die wesentlichen Unterschiede zwischen Stanzpressen und CNC-Systemen?
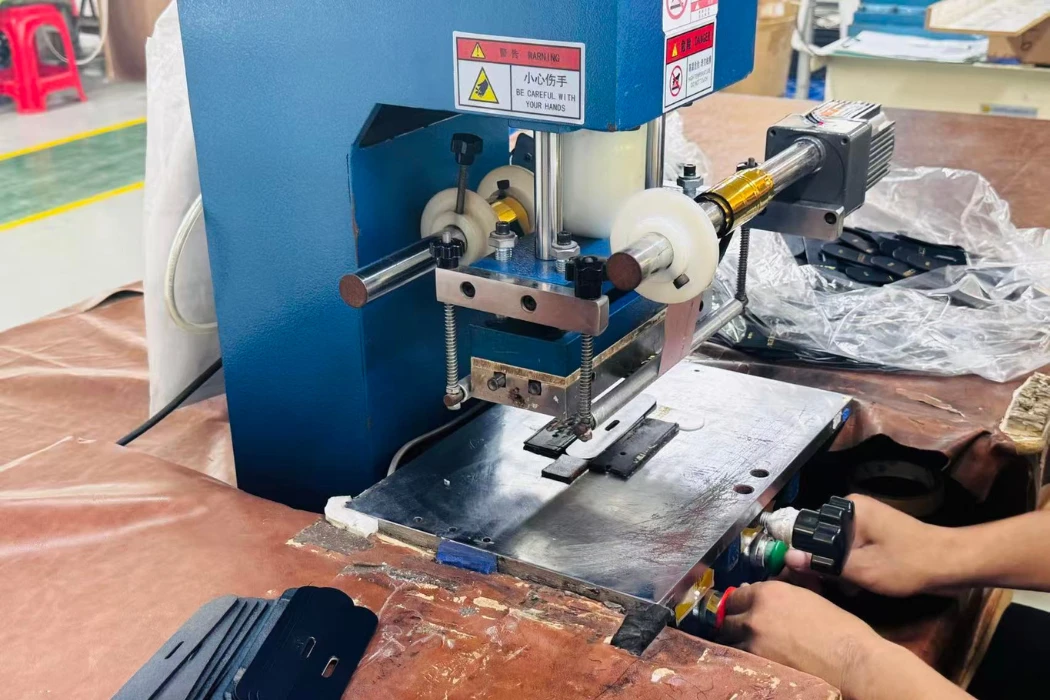
The core distinction is how the cutting path is formed: a physical die establishes the outline in die cutting, while a digital file guides the tool in a CNC workflow. Machine configuration and automation vary within both groups.
Die Mechanik einer hydraulischen Klickpresse
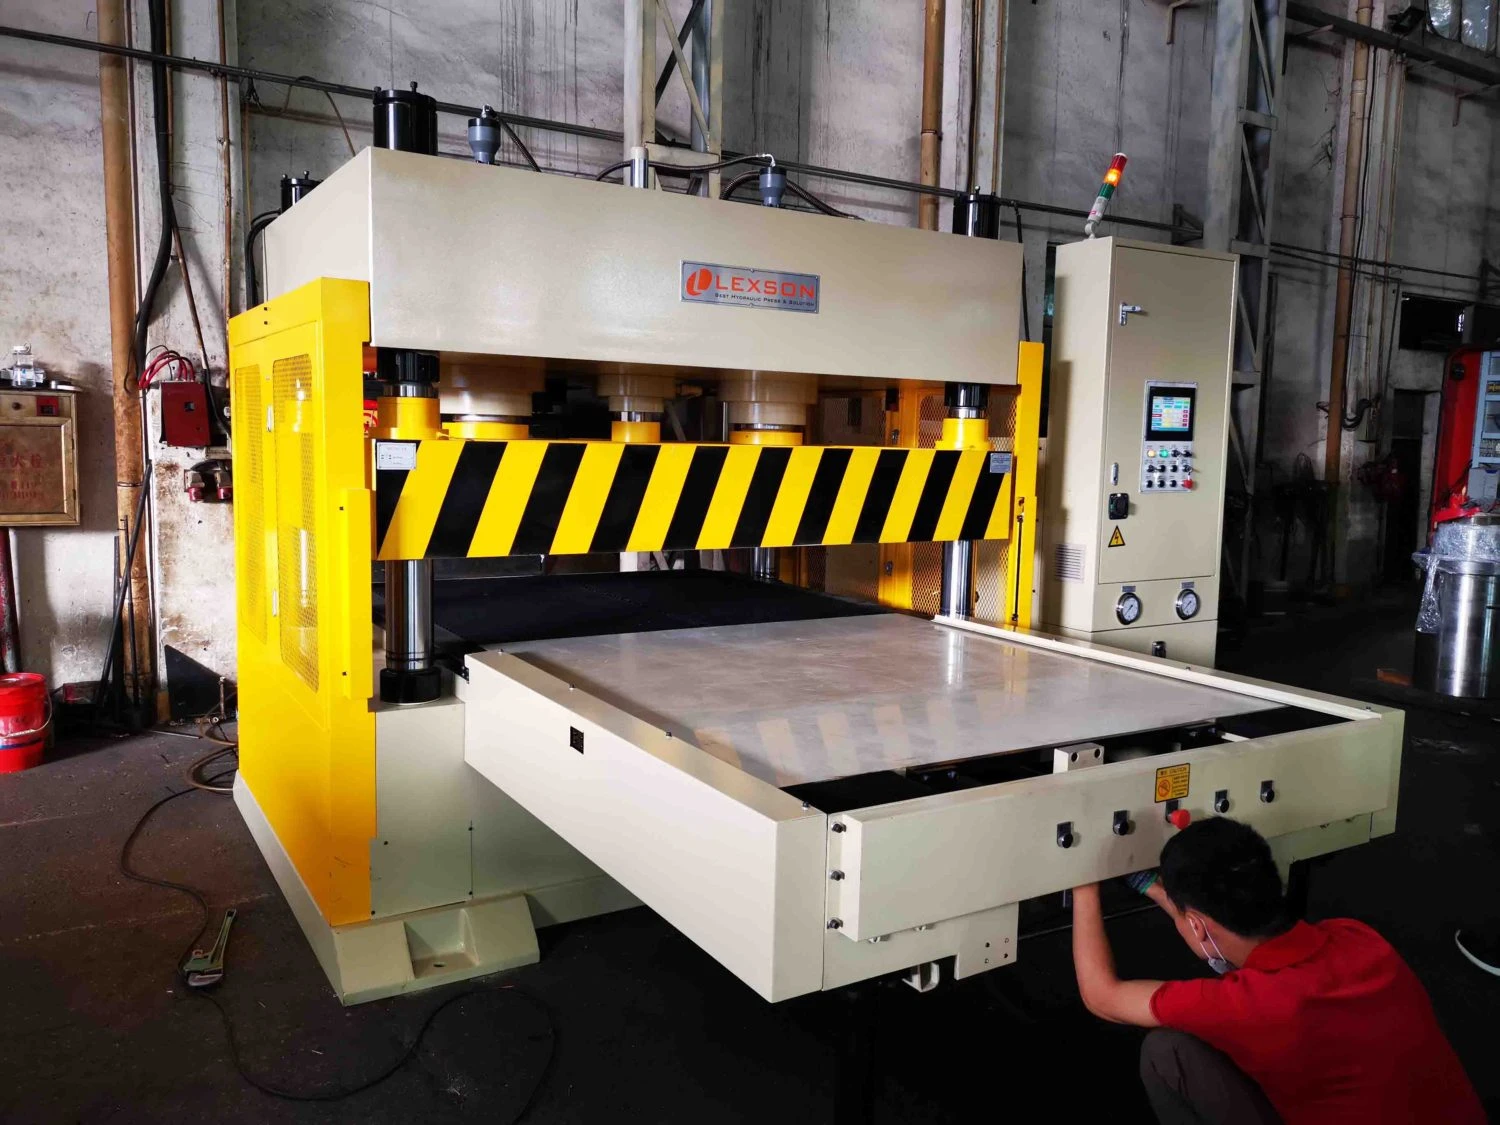
A sharpened cutting die is positioned over material supported by an appropriate cutting surface. The press supplies the force needed to drive the cutting edge through the material. Calling this only “blunt crushing” overlooks the role of the sharp die.
Press capacity, head arrangement, die size and material thickness must be compatible. Controls and safe operating sequences vary by model; follow the manufacturer’s operating procedure. ATOM’s leather-goods range includes both die-cutting and digital systems.
Wie die CNC-Digitalschneidtechnologie funktioniert
A digital cutter reads the programmed geometry and follows the tool path with a compatible cutting tool. An oscillating knife is one option, not the definition of every CNC cutter. Zünd’s tool range illustrates different knife, punching and marking options.
Material hold-down, blade selection and cutting depth affect the result. A vacuum bed can support stability, but it does not eliminate all movement or tool deflection. Oscillation frequency and stroke should be taken from the chosen tool specification, not described as one universal blade RPM.
Vergleich von Einrichtungszeit und Arbeitsablauf
A die-cutting changeover can involve locating and checking the tool, setting the machine and approving a first cut. A digital changeover can involve file preparation, nesting, tool selection, material registration and first-piece approval. Loading a file is only one part of that workflow.
Time a representative job from material loading to acceptable parts ready for the next process. Include picking, sorting and inspection. Neither a fixed die weight nor a universal seconds-per-changeover comparison is reliable across workshops.
Wie beeinflussen Schneidemethoden die Lederabfallmengen?
Hide shape, usable quality zones, part size, grain direction and assortment all affect yield. Long belt straps can impose different nesting constraints from small leather pieces. Compare systems with equivalent hides and the same acceptance rules.
Manuelles Verschachteln mit Stanzformen
An operator can inspect natural marks and place dies to meet the product’s quality requirements. Good placement involves more than filling the visible outline: stretch direction, shade and matched parts may matter. Appropriate spacing depends on the die and process.
Record why material is rejected or left unused. Some apparent waste protects product quality, while poor layouts or preventable cutting defects may be reducible. A universal gap or loss percentage cannot distinguish these causes.
Digital Nesting and Quality Mapping
Zünd’s leather workflow describes contour capture, registration of previously marked quality zones, nesting, cutting and picking. It also describes configurations in which parts are laid out manually and a camera is an upgrade. Digital cutting does not always include automatic defect recognition.
Software needs appropriate rules for orientation, quality areas and permitted spacing. An algorithm cannot make an unusable area suitable for a premium strap or guarantee that every square inch becomes a product. Validate the layout against actual material and design constraints.
Comparing Material Yield
Agree the yield definition before a trial: for example, area of accepted cut parts divided by input material area under a consistent measuring method. Track rejected parts and material reserved for other products separately so the comparison is meaningful.
Run representative material and size mixes, then compare accepted output, labour and downstream defects. Digital nesting may improve an operation’s yield, but the improvement must be measured. It cannot be assumed to be the same percentage for all belt factories.
| Vergleichsartikel | Die-cutting workflow | Digital-cutting workflow |
|---|---|---|
| Platzierung | Operator or configured placement process | Manual, assisted or automated nesting depending on system |
| Qualitätszonen | Operator recognition and agreed rules | Mapped information and nesting rules must be reliable |
| Abstand | Validate for die, material and cutting surface | Validate for blade, material and hold-down |
| Yield evidence | Measure accepted output on representative material | Use the same material and acceptance basis |
Welches System bietet eine bessere Maßtoleranz für Riemen?
The Importance of Strap Width
Width and thickness must suit the buckle and finished edge. Excessive width may cause rubbing, while insufficient width can affect appearance or retention. The amount that matters depends on the hardware geometry, not a universal one-millimetre rule.
Set the finished-part requirement first, then allocate control to cutting and subsequent processes. Measure at defined locations and under agreed conditions. A cut blank and an edge-painted assembled belt may have different dimensions.
Clicker Press Tolerance and Tool Condition
Die geometry, sharpness, material behaviour, cutting-board condition and machine setup affect dimensions and edges. Inspect the tool and sample output rather than assigning every steel-rule die the same tolerance or deflection.
Use first-piece checks and appropriate in-process sampling. Investigate a change in cut quality before continuing a long run. Tool maintenance should follow the die and machine supplier’s guidance; not every damaged die is suitable for resharpening.
CNC Precision and Finished-Part Results
Positioning accuracy in a machine specification is different from the achieved tolerance in leather. Blade wear, hold-down, material movement and path settings can affect the cut. Digital systems do not eliminate every source of physical variation.
Request a cutting trial with the intended thickness, temper and geometry. Measure actual parts after relevant handling and finishing. Confirm the result across the working area and repeat runs rather than claiming every first and thousandth belt is automatically identical.
Beeinflussen Wartungs- und Werkzeugkosten Ihr Endergebnis?
Steel Rule Dies and Physical Storage
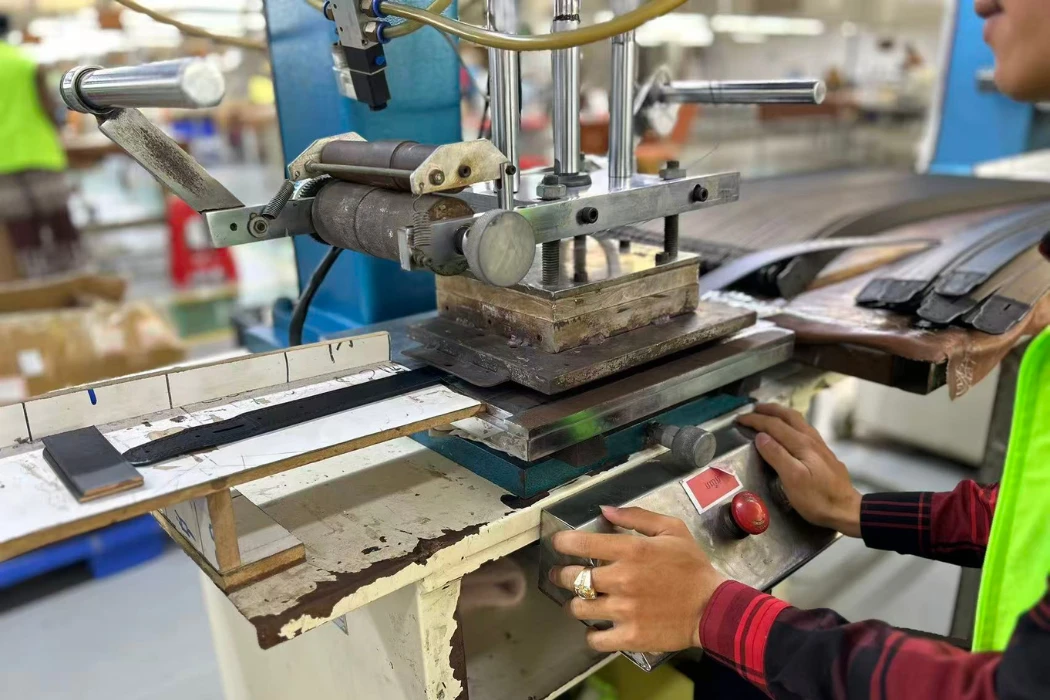
Include die design, manufacture, identification, storage, inspection and replacement in the estimate. The number of dies depends on whether the workflow cuts complete outlines or uses shared strip and end operations. Every size does not necessarily need an entirely separate full-belt die.
Agree tool ownership and access for reorders. Record condition and approved geometry, and allow for revisions when the product changes. Supplier quotations are more useful than an unsupported universal cost per die.
CNC Blades, Software and Support
Digital cutting can avoid a shaped die for each outline, but it still needs blades, cutting surfaces, tool maintenance and suitable files. Software licences, upgrades, data management, training and service may also contribute to cost.
Do not treat digital patterns as free merely because file storage is inexpensive. Preparing and checking geometry takes work. Blade type, life and replacement procedure vary with the material and machine; there is no universal price or belt count per blade.
Langfristiger Kostenvergleich
Compare installed machine cost, utilities, tooling, software, labour, service, downtime, material consumption and accepted output over the intended workload. Check what the quotation includes, including training and local support.
Use measured trial data and realistic utilisation to assess the investment. A higher purchase price can be justified in one production mix and underused in another. No generic material-saving percentage proves a rapid payback.
| Kostenkategorie | Stanzen | Digitales Schneiden |
|---|---|---|
| Installierte Ausrüstung | Machine, cutting surface, installation and support | Cutter, tools, hold-down system, software and installation |
| Produktvorbereitung | Die design or shared cutting operations | File preparation, validation and nesting setup |
| Verbrauchsmaterial | Dies and cutting surfaces | Blades, cutting surfaces and other specified consumables |
| Storage and control | Tool identification and physical storage | File/version management plus physical tools and spares |
| Economic result | Calculate cost per accepted part | Calculate on the same acceptance and workload basis |
Can Production Volume Dictate the Right Cutting Technology?
Low-Volume and Custom Runs
A small workshop may favour available die-cutting equipment for repeat shapes, while frequent revisions can make digital cutting useful even at modest volume. Material, tooling availability and the wider process determine the choice.
Compare development frequency and part variety as well as monthly quantity. Training and safe operation matter for both systems. Low purchase cost alone does not establish the lowest cost per acceptable product.
Scaling for Retail Orders
Large orders require reliable output, maintenance support and process control. Repeated simple shapes can suit die cutting, while mixed patterns and sizes may benefit from digital preparation. Neither method owns all high-volume work.
Look for representative capacity evidence and a plan for bottlenecks, breakdowns and quality checks. Review material use and responsible belt manufacturing separately from unsupported claims that one machine is automatically sustainable.
Hybrid Cutting Floors
A facility may allocate different parts to different equipment. Long straps, shaped tips, keepers and decorative pieces can have different cutting needs. A hybrid route is a production option, not proof that every sophisticated factory follows the same sequence.
Validate the interfaces between operations, including dimensions and part identification. Ask the supplier to explain the route for your design. Confirm the equipment and process proposed for the actual order, including any outsourced cutting.
Häufig gestellte Fragen zum Zuschneiden von Ledergürteln
Sind CNC-Maschinen bei der Herstellung von Ledergürteln schneller als Stanzpressen?
It depends on the shape, material, setup, loading and sorting. Compare the complete workflow and accepted output. A die may cut an outline in one stroke while a knife follows a path, but neither observation alone establishes total productivity.
Wie hoch ist die durchschnittliche Lebensdauer einer Lederstanzform?
It depends on the tool, material, cutting surface, setup and maintenance. Inspect condition and output rather than relying on a universal number of strikes. Follow supplier advice for repair or replacement.
Können CNC-Maschinen dickes, pflanzlich gegerbtes Zaumleder schneiden?
Some machine-and-tool combinations can process thick leather. Confirm the manufacturer’s capability and trial the actual material. A generic thickness claim does not cover every temper, coating or tool configuration.
Wie viel Leder wird beim Einsatz einer Klickerpresse verschwendet?
There is no universal percentage. Hide quality, shape, part dimensions and placement rules determine usable yield. Measure accepted parts on a consistent area basis and distinguish unavoidable offcuts from preventable rejects.
Do you need a skilled operator for a CNC leather cutter?
Yes. File preparation, material assessment, setup, tool checks and safe operation still require competence. Automation changes the work but does not remove responsibility for verifying the result.
Welches Schneidverfahren erzeugt sauberere Bandkanten?
Both can produce suitable edges with correct tools and setup. Compare cuts on the actual leather and inspect after the intended finishing process. Do not assume that all die cuts crush the edge or all digital cuts are defect-free.
Choosing a Cutting Route for Your Belt Programme
Define the finished dimensions and appearance first, then compare measured cutting results, accepted yield and total cost. The right route should support your design and quantity rather than a generic equipment ranking.
For Hoplok Maßanfertigung von Ledergürteln, share the drawings, material, buckle and volume so the production route can be confirmed. Leather belt MOQ is 300 units and PU belt MOQ is 1,000 units; samples take 2–3 weeks and bulk production 60–90 days, with the agreed development and approval schedule confirmed in the quotation.